A leak in a concealed PP-R joint raises a practical question: did the failure originate in fusion, material condition, handling or service loading? Before assigning responsibility, preserve the failed part and the installation records. The following checks help organise that investigation; they do not determine liability on their own.
Heating, insertion, cleanliness, alignment and cooling all affect a socket-fusion joint. Inspect these alongside the pipe condition and service history. A cut section can reveal incomplete engagement, gaps or bore restriction, but neither its colour nor the elapsed time to leakage provides a conclusive diagnosis.
Key takeaways
- A correctly fused PP-R socket joint contains no O-ring. Leakage alone does not establish whether the cause is incomplete fusion, material damage or service loading.
- A commissioning pass records the result of that test. A later leak still requires investigation of fusion quality, handling, material condition and service loads; timing alone does not identify the cause.
- Manufacturer tables vary with the system and pipe construction. The RAKtherm reference below gives OD 32 mm as 16.5 mm depth and 8 seconds of heating; it is not an approved Hitze chart.
- RAKtherm specifies a 50% heating-time increase for its outdoor work below 5 °C. Check the installed system’s instructions before applying any cold-weather adjustment.
- Map failures by location, crew, installation date, diameter and material batch. Patterns guide the investigation but do not establish the cause or liability.
On this page
- Six checks for fusion defects and process errors
- What leak timing can and cannot tell you
- What each defect looks like when you cut it open
- Manufacturer parameters and their limits
- Was it the weld, the handling or the pipe?
- Corrective action: what to do with the joints you have
- What to do next
- Frequently Asked Questions

Six checks for fusion defects and process errors
Almost every article on this subject gives you the same four-item list: too hot, too cold, dirty, twisted. That list is not wrong, but it is not diagnostic — it does not tell you which one you are holding. The following six checks cover several overlapping fusion defects and process errors.
- Cold joint. The interface never reached fusion temperature for long enough. Two pieces of plastic are touching, pressed together, and holding by friction and a partial bond.
- Overheated joint. Too much heat, or too long on the iron. Excess heat or insertion can displace melt and restrict the bore. Appearance alone does not establish thermal degradation or joint strength.
- Insufficient insertion. The pipe did not reach the installed system’s specified welding depth, leaving less fused engagement than required.
- Contaminated socket. Dust, oil, swarf or water sat on one of the two faces. The polymer could not interdiffuse across the contaminated patch.
- Wrong dwell at low ambient. The crew used summer timings in winter conditions. The result is a cold joint by a different route, which matters because the fix is different.
- Over-insertion with an intruding bead. The pipe was driven past the stop, and displaced melt has formed a ridge standing proud into the flow area.
A correctly made PP-R socket joint bonds the pipe and fitting without an O-ring or gasket. A leaking fused connection has no mechanical seal to tighten. Determine the cause and use the repair method approved for the installed system; replacing the affected section may be necessary. The presence of a leak does not prove that fusion never occurred.
What leak timing can and cannot tell you
Record whether leakage appeared during filling, commissioning or later service, together with the pressure, temperature and loading history. Use timing to decide which records to examine. There is no verified failure dataset here that assigns a particular defect to a month or year of service.
Leakage during filling or commissioning. Check the joint engagement, evidence of damage, alignment and the test setup. Inspect the leak path before discarding the part. The result establishes failure under those test conditions, but it does not by itself separate a fusion defect from damaged material or an installation load.
Leakage after commissioning. Preserve the original test record and compare it with the later service conditions. Check for incomplete fusion, contamination, handling damage and loading. Passing a pressure test does not identify what caused a subsequent leak, and the time between the two events does not supply that missing evidence.
Build a failure map before choosing the remediation scope. Include both leaking and inspected non-leaking locations, pipe and fitting batch marks, crew records and service changes. This helps select additional samples without assuming that every joint in a group has the same defect.
| Defect | Evidence to check | Possible observation; verify cause |
|---|---|---|
| Cold joint | Heating and change-over records | Gaps or interface separation; colour alone is inconclusive |
| Overheated / collapsed bore | Heating, insertion and flow observations | Displaced melt or narrowed bore; strength needs separate assessment |
| Insufficient insertion | Insertion mark and engagement depth | Compare engagement with the installed system’s required depth |
| Contaminated socket | Heating and change-over records | Foreign matter may support a contamination hypothesis |
| Wrong dwell at low ambient | Ambient conditions and approved timing adjustment | Assess with weld records; date alone cannot diagnose the joint |
| Over-insertion / intruding bead | Insertion depth and bore inspection | Internal bead standing proud into the bore |
Source: investigation checklist based on the manufacturer preparation and assembly guidance discussed below. These observations are hypotheses to check, not pass/fail criteria or failure-frequency data.
What each defect looks like when you cut it open
Preserve the failed joint and its location record before making a longitudinal section through the suspected leak path. Follow the agreed investigation method so cutting does not obscure the evidence. Inspect engagement, gaps, deformation and foreign material; do not use the number of visible colours as a bond test.
Investigate an incomplete-fusion hypothesis. Look for a gap or separation along the contact area and compare it with the welding record and the installed system’s assessment method. A visible line or colour change alone is insufficient. SIMONA’s welding guide states that compatible materials of different colours can still weld together.
Investigate displaced melt and bore restriction. Record a narrowed bore, irregular bead or deformation. Excessive heat or insertion can displace material. These observations warrant checking the tool temperature and assembly depth, but appearance alone does not establish thermal degradation or load-bearing strength.
Check engagement against the correct reference. Measure the socket engagement and compare it with the installed system manufacturer’s depth requirement. The RAKtherm table below illustrates what a named reference looks like; it cannot establish the required depth of a Hitze fitting or another manufacturer’s socket.
Preserve evidence of contamination. Record foreign matter on the contact area before cleaning or destructive examination. Compare that observation with preparation records. A smooth, torn or fibrous surface alone cannot determine the cause or certify that the remaining joint was sound; use the applicable assessment method for that conclusion.
Manufacturer parameters and their limits
Use a timing and depth chart approved for the installed pipe and fitting system. The table below reproduces RAKtherm’s PP-R reference for OD 20–110 mm, from its 2023 catalogue, Table 4.1. RAKtherm describes it as guidance according to DVS 2207 part 11. The values belong to that manufacturer’s instructions; they are not a universal DVS table or a Hitze commissioning instruction.
| Pipe OD (mm) | Welding depth (mm) | Heating (seconds) | Welding time (seconds) | Cooling (min) |
|---|---|---|---|---|
| 20 | 14 | 5 | 4 | 2 |
| 25 | 15 | 7 | 4 | 2 |
| 32 | 16.5 | 8 | 6 | 4 |
| 40 | 18 | 12 | 6 | 4 |
| 50 | 20 | 18 | 6 | 4 |
| 63 | 24 | 24 | 8 | 6 |
| 75 | 26 | 30 | 8 | 8 |
| 90 | 29 | 40 | 8 | 8 |
| 110 | 32 | 50 | 10 | 8 |
Source: RAKtherm, PPR and PEX Catalogue (2023), printed pp. 51–53; Table 4.1 is on printed page 52. “Welding time” follows that source’s heading. Confirm the applicable assembly interval, cooling conditions and current procedure with the installed system manufacturer.
The reference shows why one remembered heating time cannot cover every size. RAKtherm lists 5 seconds at OD 20 mm and 40 seconds at OD 90 mm. Before applying a figure, confirm the pipe construction and the current procedure. SIMONA’s separate guidance distinguishes SDR 11 from SDR 17 and gives different cooling values for some diameters; combining the two tables would hide their limits.
Check these additional fields in the system’s approved procedure:
- Setpoint. SIMONA’s heated-element socket guidance gives 260 ± 10 °C and requires instrument verification of tool temperature. Its PP butt-fusion guidance gives 210 ± 10 °C. These are named-manufacturer references, not permission to change the installed system’s approved setpoint. See SIMONA, work.info: Welding (November 2011), printed pp. 9, 15, 17 and 52.
- Change-over time. SIMONA defines the interval from separating the heated surfaces to bringing them into contact, and tabulates a maximum separately from heating and cooling. Check how the installed system’s instructions define “welding”, “processing” and “change-over” time before using a chart.
- Equipment by diameter. Use the welding equipment required by the installed system manufacturer. SIMONA specifies suitable equipment for PP from 63 mm inclusive; this does not establish a universal manual-to-machine cutoff for every PP-R system.
Cold-weather adjustment is system-specific. RAKtherm’s 2023 catalogue states that its outdoor welding below 5 °C requires a 50% increase in heating time, citing DVS 2207 part 11. That instruction changes heating, not cooling. Use the current instructions for the installed system, including any protection from weather and limits on site welding; do not apply the RAKtherm adjustment to a different product without confirmation.
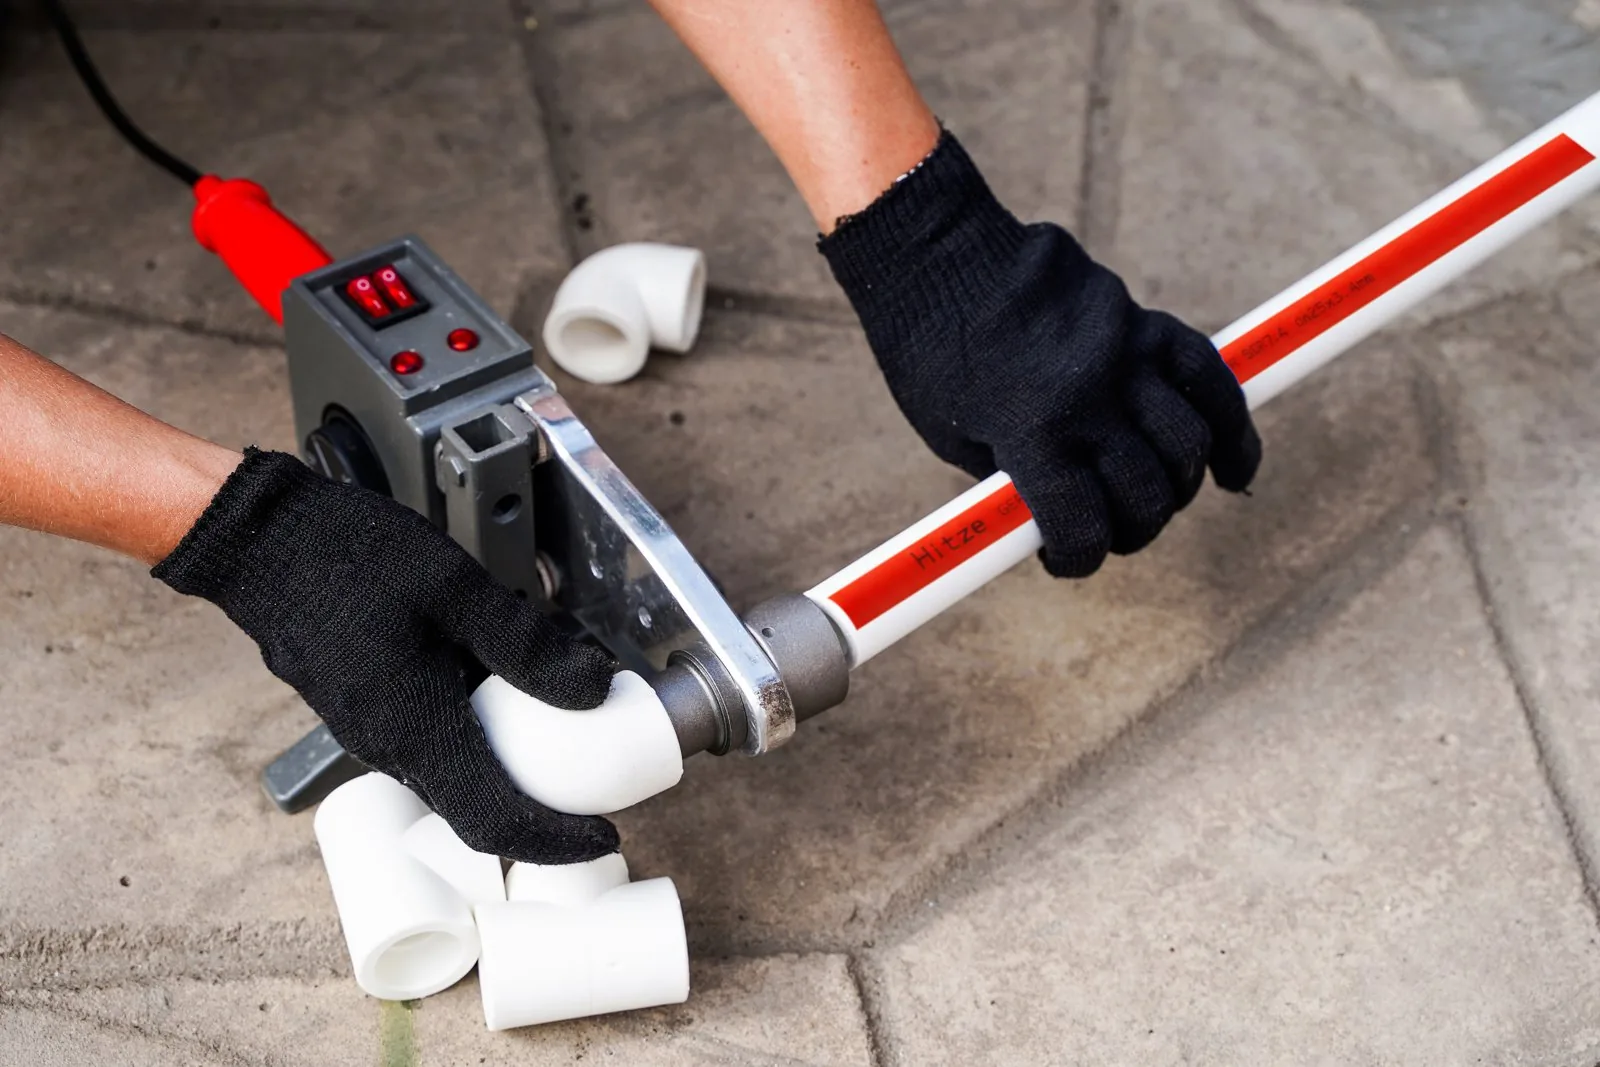
SIMONA’s socket-welding guide specifies an external chamfer of about 15°, with a width of 2 mm up to OD 50 mm and 3 mm above it. It describes joining to the mark or stop without distortion or tilting, followed by clamping and cooling. These details belong to that guide; check the installed PP-R system’s preparation and assembly instructions before using them.
Follow the installed system’s depth mark or stop instruction and preserve its specified assembly interval. Do not infer correct engagement solely from the bead covering a mark. Inspect any suspected bore restriction against the fitting geometry and the manufacturer’s acceptance criteria.
Was it the weld, the handling or the pipe?
Separate observations from conclusions when investigating responsibility. Fusion records, handling conditions, material records and service loads may all matter. A pattern across the building helps choose what to inspect, but it cannot assign liability without corroborating evidence.
Investigate fusion. Map joint failures against crew, shift, diameter and installation conditions. Check the tool-temperature, heating, change-over, engagement and cooling records where available. A cluster may justify additional inspection, but crew overlap alone does not prove defective workmanship.
Investigate handling and loading. Record impact marks, exposed storage, forced alignment, support conditions and any movement during cooling. Include both joint and pipe-barrel failures. Check the approved handling and support instructions instead of treating the location of the leak as a conclusive cause.
Investigate material condition. Record the pipe and fitting batch marks and check dimensions against the relevant product documents. Material problems can affect a joint or pipe barrel and may be limited to one batch. Request the batch records and arrange the appropriate examination; this article holds no dataset ranking material defects by frequency.
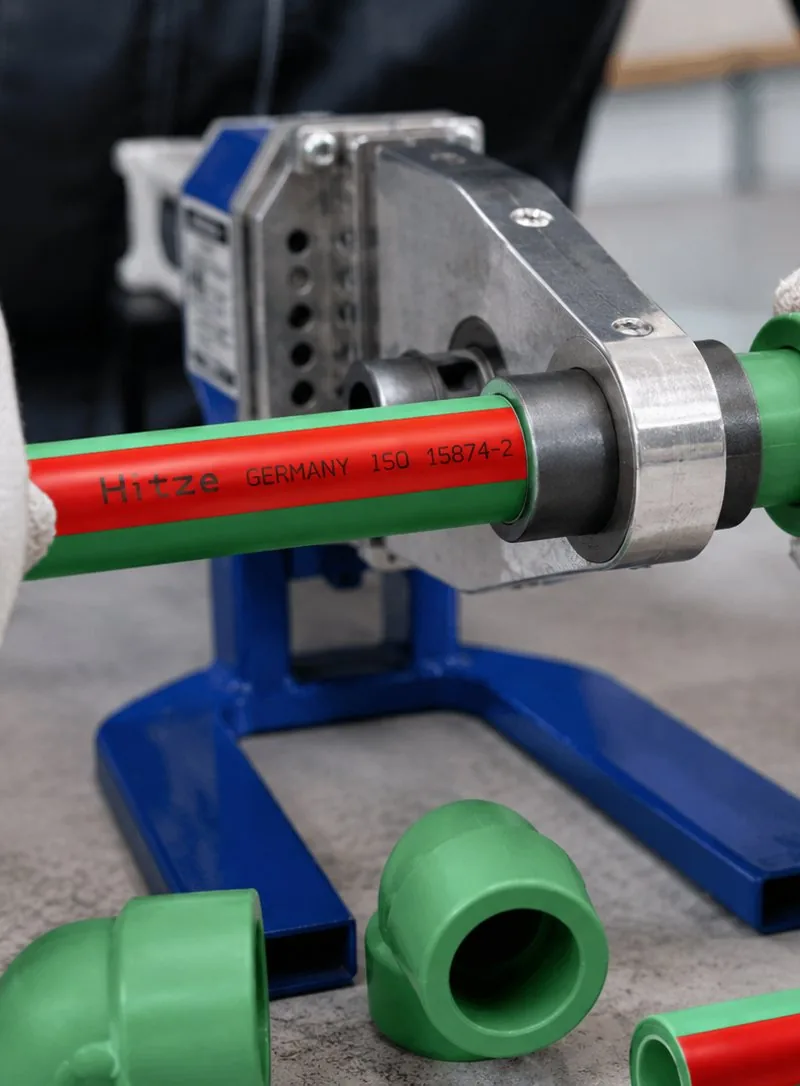
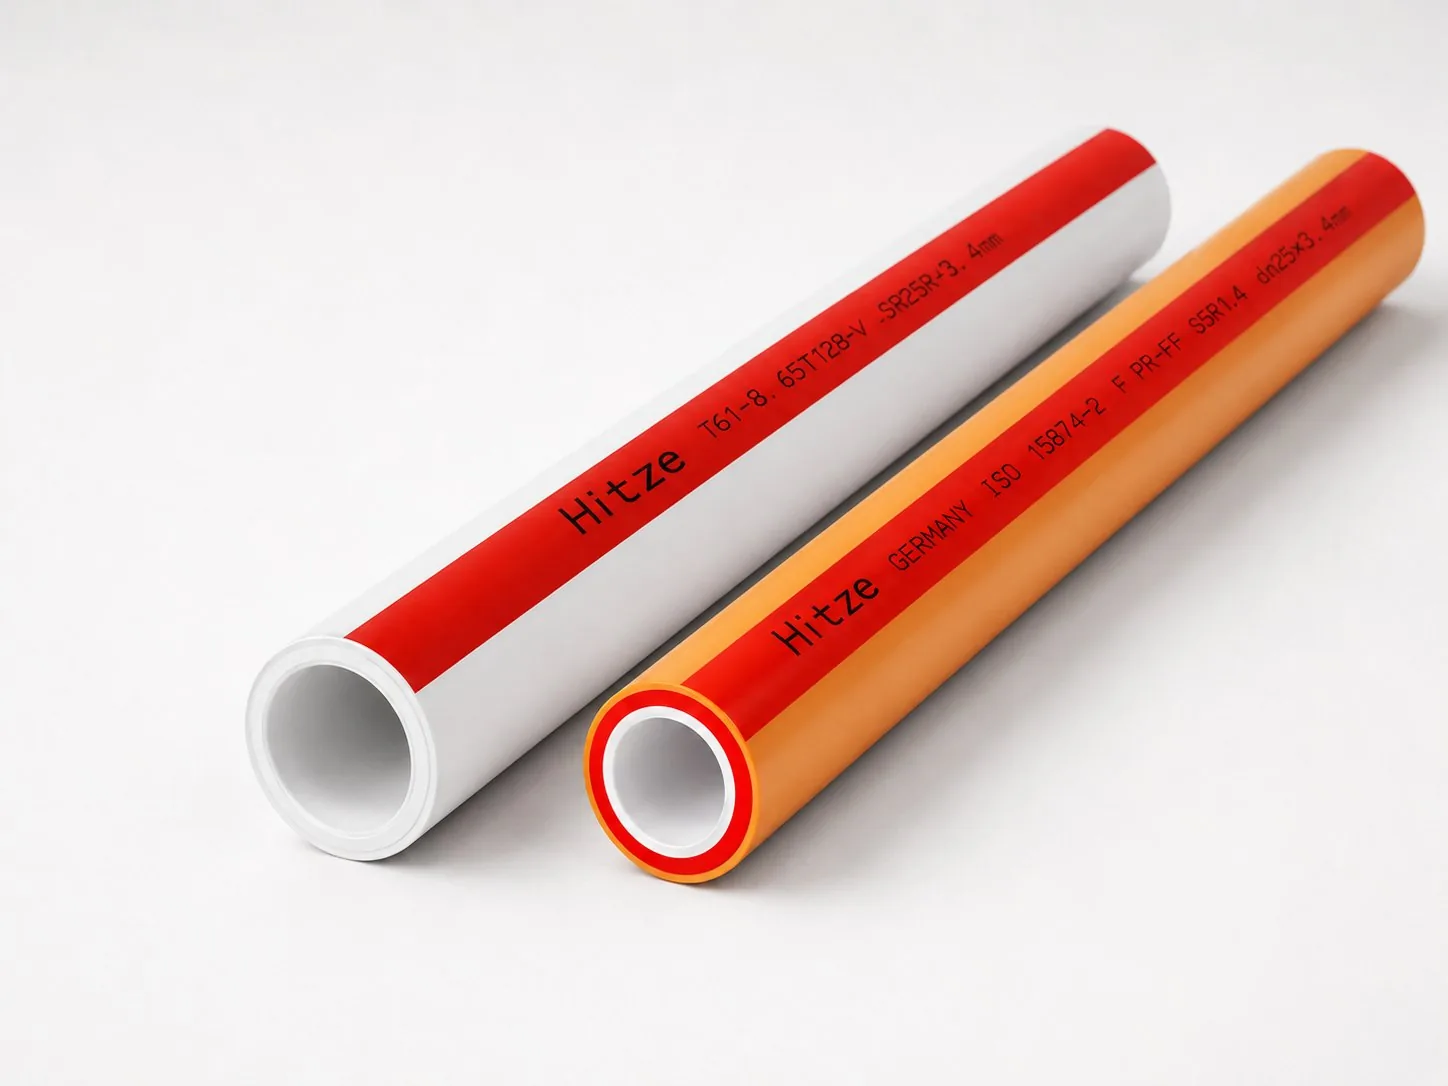
Hitze’s documented QC sequence includes resin verification before extrusion, checks of outside diameter, wall thickness and ovality, and hydrostatic testing of pipe, fittings and fused assemblies. Request the records applicable to the disputed batch rather than assuming a complete cause analysis follows from routine QC. The relevant product-standard family is discussed in EN ISO 15874 and its service classes. Compare the actual service conditions with the product rating as part of the investigation.
Before anyone repairs anything, document it. Photograph the joint in situ before removal, cut it longitudinally rather than crushing it out, keep the failed joint labelled with location and date, and record the pipe’s printed markings — the PP-R pipe and fitting print line carries the size, class and standard reference that a supplier will ask for first. A failed joint in a bin is worth nothing in a dispute.
Corrective action: what to do with the joints you have
A fused PP-R socket joint has no mechanical seal to tighten. Use the installed system’s approved repair method after assessing the cause; this may require cutting out the affected section and installing a replacement fitting. Keep the removed joint as evidence and agree the extent of remediation before concealing the pipework again.
Scope the population, not only the leak. Map the failed joint to the installation records, then select additional samples under the project’s investigation plan. Replacing only the leaking connection can leave other suspect joints in service. Use the inspection findings to decide the remediation extent rather than assuming that all joints in a crew’s work share a defect.
Then re-test to the approved PP-R system procedure. Agree the test method with the system manufacturer and the project specifier before testing. Record the applicable document and revision, test medium, pressure, stabilization period, hold duration and acceptance criteria. Use the procedure approved for the installed pipe and fitting system; a sequence copied from another manufacturer’s manual is not a Hitze commissioning instruction.
A pressure-test guide for alpex multilayer pipe and its crimp or push-fit connectors cannot establish the test pressure or hold time for a socket-fused PP-R installation. Its reference to EN 806-4 does not make its product-specific figures transferable. For a project using that standard, confirm the applicable test method against the current standard and the PP-R manufacturer’s instructions rather than adopting the alpex values.
Work to the applicable system procedure and project specification, and record which document and revision you used. The cited alpex guide separates compressed-air and water tests; its timings do not establish a commissioning procedure for the installed PP-R system.
Allow the test medium and pipework to reach thermal equilibrium before recording the pressure trend. Select a calibrated gauge with the resolution required by the approved procedure, and keep joints visible for inspection. Detailed test sequencing belongs to the system’s commissioning instructions. A short test or an unstable temperature cannot establish the long-term integrity of a suspect fusion joint.
Prevent recurrence using the verified cause. Check insertion references, per-size heating and assembly intervals, actual tool temperature, required equipment and cooling restraint against the approved procedure. Confirm any cold-weather adjustment with the installed system manufacturer. Document the corrected method and check its use at the workface before returning the installation to service.
If the diagnosis lands on the material side, or if repeated failures make you doubt the supply rather than the crew, that is a sourcing question rather than a site one — the specification, certification and batch-documentation side is covered on the distributor and importer supply pages, and the practical comparison of joint methods by diameter sits in the fusion welding methods guide. The procedure itself — the correct sequence rather than its failure modes — is covered in how to weld PP-R pipe, and the material’s broader behaviour, including why a fused joint is an advantage in the first place, is set out in PP-R advantages and disadvantages.
What to do next
If you are holding a failure, preserve and label it before repair. Inspect engagement, gaps, deformation and foreign matter using the agreed assessment method; colour alone is inconclusive. Compare measurements with the installed system’s instructions. Map locations to crew, date, diameter and batch records, select further samples under the investigation plan, and agree the repair extent. Re-test with a calibrated gauge whose resolution matches the approved system procedure.
On specification and supply, what you can reasonably establish before ordering: PP-R is available in an OD 20–110 mm range for the Hitze line, standards scope for the range is documented against DIN 8077/8078 and EN ISO 15874 with SKZ testing and DVGW type examination for drinking-water pipe — ask any supplier for the certificate reference and the models each one covers rather than accepting a logo.
Confirm current minimum-order terms, sample availability, sample and production lead times, quotation inclusions and exclusions, and the records needed to verify the production batch in writing before ordering. If you are specifying rather than repairing, the specification and submittal checklist is the shorter route.
Frequently Asked Questions
Can a leaking PP-R fusion joint be repaired without cutting it out?
A fused socket joint has no mechanical seal to tighten. Follow the installed system’s approved repair method; it may require removing the affected section and installing a replacement fitting. Preserve the failed part before repair.
Why can a joint pass commissioning and leak later?
A pass records the outcome under the commissioning test conditions. A later leak requires investigation of fusion quality, material condition, handling and service loads. Elapsed time alone cannot identify which caused the failure.
How deep should PP-R pipe go into the fitting?
Use the installed pipe and fitting system’s approved welding depth. As a named reference only, RAKtherm’s 2023 Table 4.1 lists 14 mm at OD 20, 16.5 mm at OD 32, 24 mm at OD 63 and 32 mm at OD 110. These figures are not a Hitze depth chart.
What changes when welding PP-R in cold weather?
Follow the installed system’s current weather and temperature instructions. RAKtherm’s 2023 catalogue specifies 50% more heating time for its outdoor welding below 5 °C. Confirm applicability before using that adjustment on another system.
How can I tell a fusion defect from a faulty batch of pipe?
Compare joint observations with the welding, handling, service and batch records. Map locations, crew, date, diameter and material batch to guide further inspection. Clustering or failure location alone cannot establish cause or liability.
Is an oversized weld bead a sign of a strong joint?
Bead size alone cannot establish strength or thermal damage. Displaced melt or a restricted bore warrants comparison with the fitting geometry, welding record and applicable acceptance criteria.
Which equipment is required for larger PP-R sockets?
Use the equipment required by the installed system manufacturer for the diameter and construction. SIMONA specifies suitable equipment for PP at 63 mm and above; that statement does not establish one manual-to-machine cutoff for every PP-R system.