Key takeaways
- The profile is chosen by the fitting maker, not by you. Each press fitting is engineered and certified around one pressing contour. Press it with the wrong jaw and you deform the wrong zone — the joint can look pressed yet fail the manufacturer’s design and void the approval.
- TH, U, F and H are the composite-pipe contours; M, V and SV are the metal-press contours. Multilayer PEX-AL-PEX and PE-RT use TH/U/F/H. Copper, stainless and carbon steel use M/V. They are not interchangeable across those two worlds.
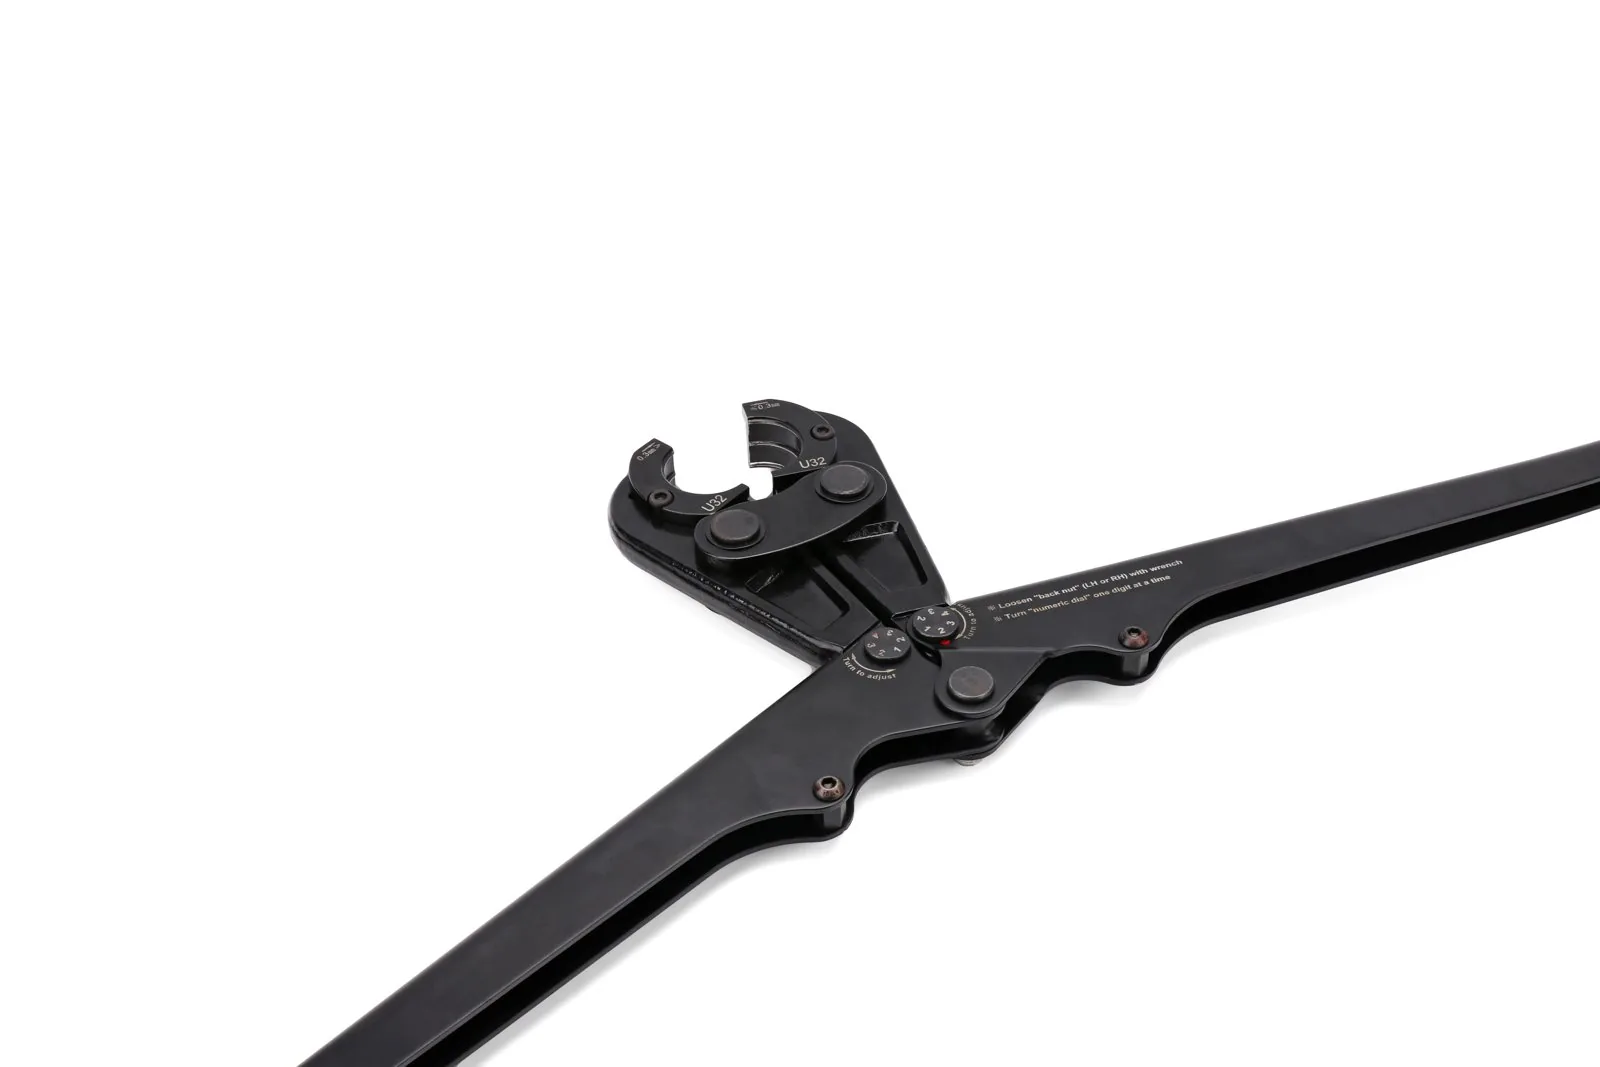
- Your press gun is not the lock-in — the jaw is. Novopress, REMS, Klauke, Ridgid and Milwaukee bodies all accept swappable jaws and rings by profile and diameter. A contractor rarely needs a new machine, only the right jaw.
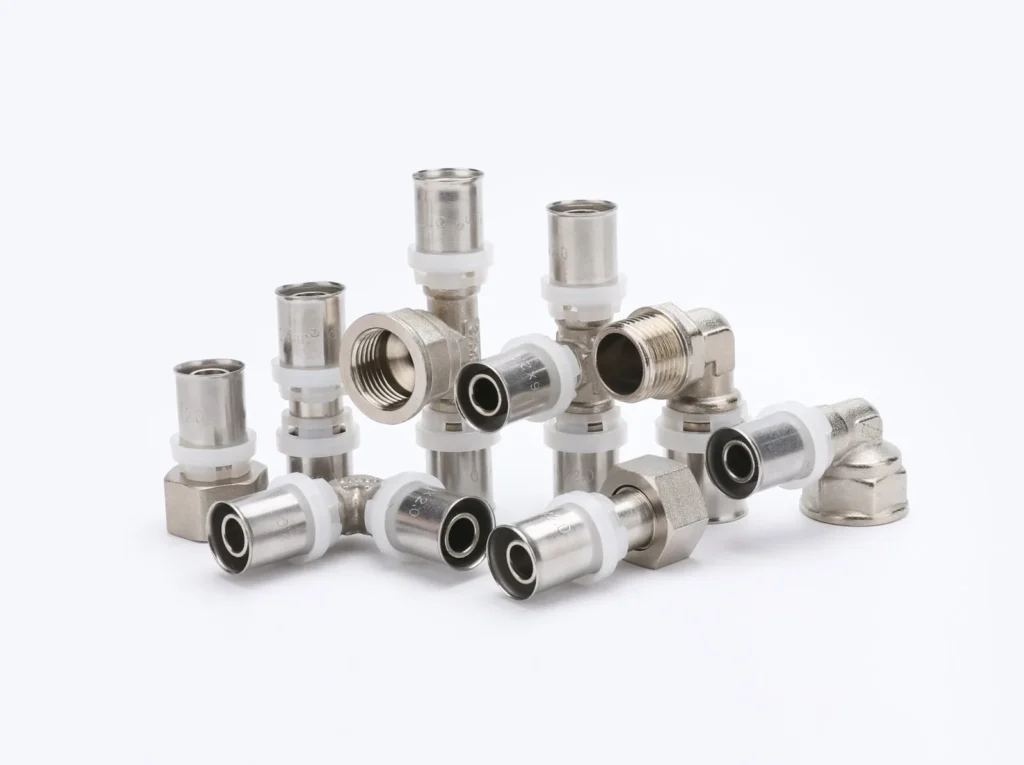
- Hitze press fittings are offered in TH, U, F and M profiles, built with a lead-free brass bore, stainless sleeve and twin O-ring seal — so you can standardise on one supplier without re-tooling the crew.
What a “jaw profile” actually is — and why the wrong one fails silently
A press-fitting jaw profile is the shape stamped into the tool jaw (or press ring) that closes around the fitting sleeve and squeezes it onto the pipe. The letters — TH, U, F, H, M, V — describe the geometry of that contour: where the jaw contacts the sleeve, how many compression bands it forms, and where the load is concentrated relative to the O-ring underneath. It sounds like a small detail. On a job site it is the difference between a joint you can warrant and a callback you pay for out of pocket.
Here is the part every fitting manufacturer and independent tooling guide agrees on, and the single most important sentence in this article: the correct jaw profile is determined by the fitting manufacturer, not by the installer. Each fitting is designed and tested with one specific pressing contour, and the certification approval is tied to that contour. Mix a TH fitting with a U jaw of the same diameter and the tool will still close — that is the trap. The visible crimp can look acceptable while the O-ring is compressed unevenly, the sleeve is deformed in the wrong plane, and the joint no longer matches the geometry it was leak-tested to. It may hold at commissioning pressure and weep six months later behind a finished wall. There is no field method to “check” a mis-profiled press after the fact; the only defence is matching the contour before you pull the trigger.
That is why “will these fittings work with my press tool?” is really two questions. First: does my tool accept a jaw or ring in the profile this fitting requires? Almost always yes. Second: is that jaw sized for this exact diameter? Also usually yes, once you own the set. The profile question is the one that decides warranty; the diameter question decides whether today’s install can happen. Get both right and the brand on the fitting is your choice, not your tool’s.
TH, U, F, M: which profile belongs to which system
The four profiles a multilayer and mixed-material contractor meets most often each carry a lineage. Knowing that lineage tells you instantly whether a fitting will fit the jaws already in your case.
TH profile is the most widely adopted composite-pipe contour in Europe. It is used across a long list of multilayer systems — Viega, Wavin, Unipipe/Unicor, Henco, Comap/Purmo and Tiemme among them. If your crew already presses multilayer PEX-AL-PEX from a European brand, there is a strong chance TH jaws are already in the kit. TH’s breadth is precisely why it is the safest default to standardise around for a mixed fleet of installers.
U profile is associated with Uponor and its compatible lines (Unicor Unipipe, Wavin Tigris, Coes). U-profile jaws are made for the mainstream tool bodies — Ridgid, REMS, Klauke, Novopress — so a contractor moving between an Uponor-spec job and a general multilayer job usually only swaps the jaw, not the gun. If your radiant-heating work leans on Uponor-style systems, U is the contour to confirm on any new fitting supplier.
F profile (F-contour) originates with Fränkische’s alpex multilayer system. It matters here for one genuinely useful reason: Fränkische’s own alpex-duo XS fittings are engineered to be pressed with both F- and TH-contours using conventional certified press tools. That is a rare, manufacturer-stated dual approval, and it is worth knowing because it shows contour flexibility is designed in at the fitting, never improvised at the jaw. Do not read it as licence to cross profiles freely — it is an approval that exists only because that specific fitting was tested for it.
M profile lives in a different material world. M is the system-independent contour for metal press systems — copper, stainless steel and carbon steel — used by brands such as Geberit, Sanha and Conex Bänninger’s >B< Press, and by drinking-water metal fittings governed by DVGW worksheet W 534. Because M is system-independent, any M-contour fitting can be pressed with any M-contour jaw. That is the exact opposite of the composite world, and the reason you must never assume a plastic-composite habit carries over to metal. V profile is the parallel copper contour (Viega Profipress and similar), used for copper and some gas and heating lines.
The compatibility table contractors actually need
This is the reference to keep on the van. It maps each profile to the pipe world it belongs to, the systems it is associated with, and the practical rule. Treat the “associated systems” column as a lineage guide, not a licence — always confirm the specific fitting’s approved contour on its own data sheet before you press.
| Profile | Pipe / material world | Associated systems | Practical rule |
|---|---|---|---|
| TH | Multilayer composite (PEX-AL-PEX, PE-RT-AL) | Viega, Wavin, Henco, Unipipe/Unicor, Comap Purmo, Tiemme | Widest composite contour — safest fleet default. |
| U | Multilayer composite | Uponor, Unicor Unipipe, Wavin Tigris, Coes | Jaws run on Ridgid/REMS/Klauke/Novopress — swap jaw, keep gun. |
| F | Multilayer composite | Fränkische alpex (some fittings dual-approved for F and TH) | Dual approval only where the maker states it — never assumed. |
| H | Multilayer composite | Roth, Valsir, Aquatechnik, Prandelli lines | Less common — verify jaw availability before you spec. |
| M | Metal press (copper, stainless, carbon steel) | Geberit, Sanha, Conex >B< Press; DVGW W 534 drinking-water | System-independent — any M jaw presses any M fitting. |
| V | Metal press (copper, gas, heating) | Viega Profipress and similar copper systems | Copper contour — do not confuse with composite habits. |
Read the table with one discipline in mind: the columns for composite (TH/U/F/H) and metal (M/V) never bleed into each other. A crew that has pressed copper with M jaws for a decade will instinctively “just press” a multilayer fitting — and that instinct is exactly how a mis-profiled joint gets into a wall. Composite fittings for water and radiant heating that Hitze supplies are built to EN ISO 21003-3, the fittings part of the multilayer piping standard, and the pressing contour on the fitting is what carries that approval into the field.
The table above tells you which world a contour lives in. The one below is the purchasing version: for each profile, the pipe it presses, the diameter band you can actually buy jaws and rings for, and which tool bodies accept that jaw. Diameter bands are the jaw/ring ranges published by the tool and system makers, not a promise about any one fitting range — confirm the sizes on the fitting data sheet.
| Profile | Pipe it presses | Jaw / ring band (mm OD) | Tool bodies that take this jaw | Note before you buy | ||||
|---|---|---|---|---|---|---|---|---|
| TH | Multilayer PEX-AL-PEX / PE-RT-AL | 14–63 (jaws to 32, rings above) | REMS, Novopress, Rothenberger, Klauke, Milwaukee, Ridgid | U | Multilayer (Uponor MLC / Uni Pipe lineage) | 14–63 (Uponor S-Press PLUS fittings 16–32) | Uponor UP110 / Mini2, REMS, Novopress, Klauke, Milwaukee, Ridgid, Hilti | Uponor’s own tools are the reference; third-party bodies are listed in its compatibility matrix. |
| F | Multilayer (Fränkische alpex lineage) | 16–63 (F-contour jaws) | Fränkische-branded jaws sold to fit mainstream 32 kN bodies | alpex-duo XS is factory-approved for both F and TH — a stated exception, not a rule. | ||||
| M | Copper, stainless, carbon steel (Mapress, >B< Press, Sanha) | 12–108 (jaws 12–35, collars/slings 42–108) | Novopress, REMS, Rothenberger, Milwaukee, Bosch, Hilti, Viega Pressgun (per Geberit 2025 list) | System-independent contour; Conex >B< Press chart: 15–28 mm "press jaws only, slings not permitted". | ||||
| V | Copper (Viega Profipress lineage), gas and heating | 12–108 (Profipress approved d12–108) | Viega Pressgun, REMS, Novopress, Klauke, Ridgid, Milwaukee | Viega SC-Contur: an unpressed V joint leaks visibly at 1–6.5 bar (water) or 22 mbar–3 bar (air). |
Your press gun is not the lock-in — the jaw is
The most expensive misconception in press systems is that changing fitting brands means buying a new tool. For the overwhelming majority of contractors, it does not. The major press-tool platforms — Novopress, REMS, Klauke, Ridgid and Milwaukee — are built around interchangeable jaws and press rings. The gun supplies the force; the jaw supplies the contour. Change the jaw, and the same battery-powered body that pressed one brand yesterday presses another today, provided the jaw matches both the profile and the diameter of the fitting.
That has a direct commercial consequence. A distributor or a fit-out contractor who has been paying a premium to a single brand — often a Viega or Uponor system — because “the crew’s tools only take those fittings” is usually mistaken. The tools take the profile. If a comparably certified fitting is available in that same TH or U contour, the switch costs a set of jaws, not a fleet of guns. That is the entire economic argument for standardising on a full-range supplier: you keep every press gun on the truck and change only the consumable at the tip.
There is one honest caveat. A handful of manufacturers ship proprietary or “system” jaws intended to keep their fittings and tools paired — some Viega Smartpress and Uponor S-Press setups lean this way. Where that is the case, you either buy the matching jaw or you spec a fitting in an open contour that your existing jaws already cover. Hitze deliberately sits on the open side of that line: its press fittings are made in the mainstream TH, U, F and M contours precisely so a trade buyer never has to re-tool a crew to adopt them. If your team already presses multilayer, you almost certainly already own the jaw that presses a Hitze fitting.
Same profile, different jaw brand: the risk nobody prices in
“Any TH jaw presses any TH fitting” is true mechanically and only partly true contractually. Three things decide whether a same-profile jaw from another brand is a safe swap, and none of them is the letter stamped on the jaw.
1. Force class. Standard radial presses are 32 kN bodies; REMS also sells a 45 kN XL body, and the mini/compact class (REMS Mini-Press, Novopress ACO102/103, Rothenberger Compact, Milwaukee M12) sits below that and carries jaw sets that stop at 28–35 mm. A jaw is cut for a force class and a pin geometry — REMS describes its tongs as fitting “suitable radial presses of other makes”, not all of them. A 32 kN jaw on a mini body does not reach the contour depth it was tested at.
2. The fitting maker’s compatibility list, and its expiry date. Approvals are granted per tool model, not per profile letter. Geberit’s current list for Mapress and Mepla names Novopress, Rothenberger, Milwaukee, Bosch, Hilti and Viega bodies — and is valid from 01.04.2025 to 01.04.2026 (edition 03-2025), with an explicit line that Geberit gives no warranty for third-party tools. Viega’s US tool matrix goes the other way: “Viega does not require the use of specific, approved tools to maintain the fitting warranty.” Two market leaders, two policies. Read the list of the fitting you are pressing, and read its date.
3. Jaw condition. A worn or cracked contour presses like the wrong contour. Novopress requires a visual check for cracks and wear before each use and a factory service at least every two years; the same discipline applies to any brand’s jaw on any brand’s body. A jaw bought second-hand with no service record is the cheapest way to put a mis-profiled joint behind a wall.
The practical rule for a mixed fleet: standardise jaws by profile and force class, keep every jaw inside a service window, and hold the fitting maker’s current compatibility sheet in the submittal file.
How a Hitze press fitting is built and what gets checked
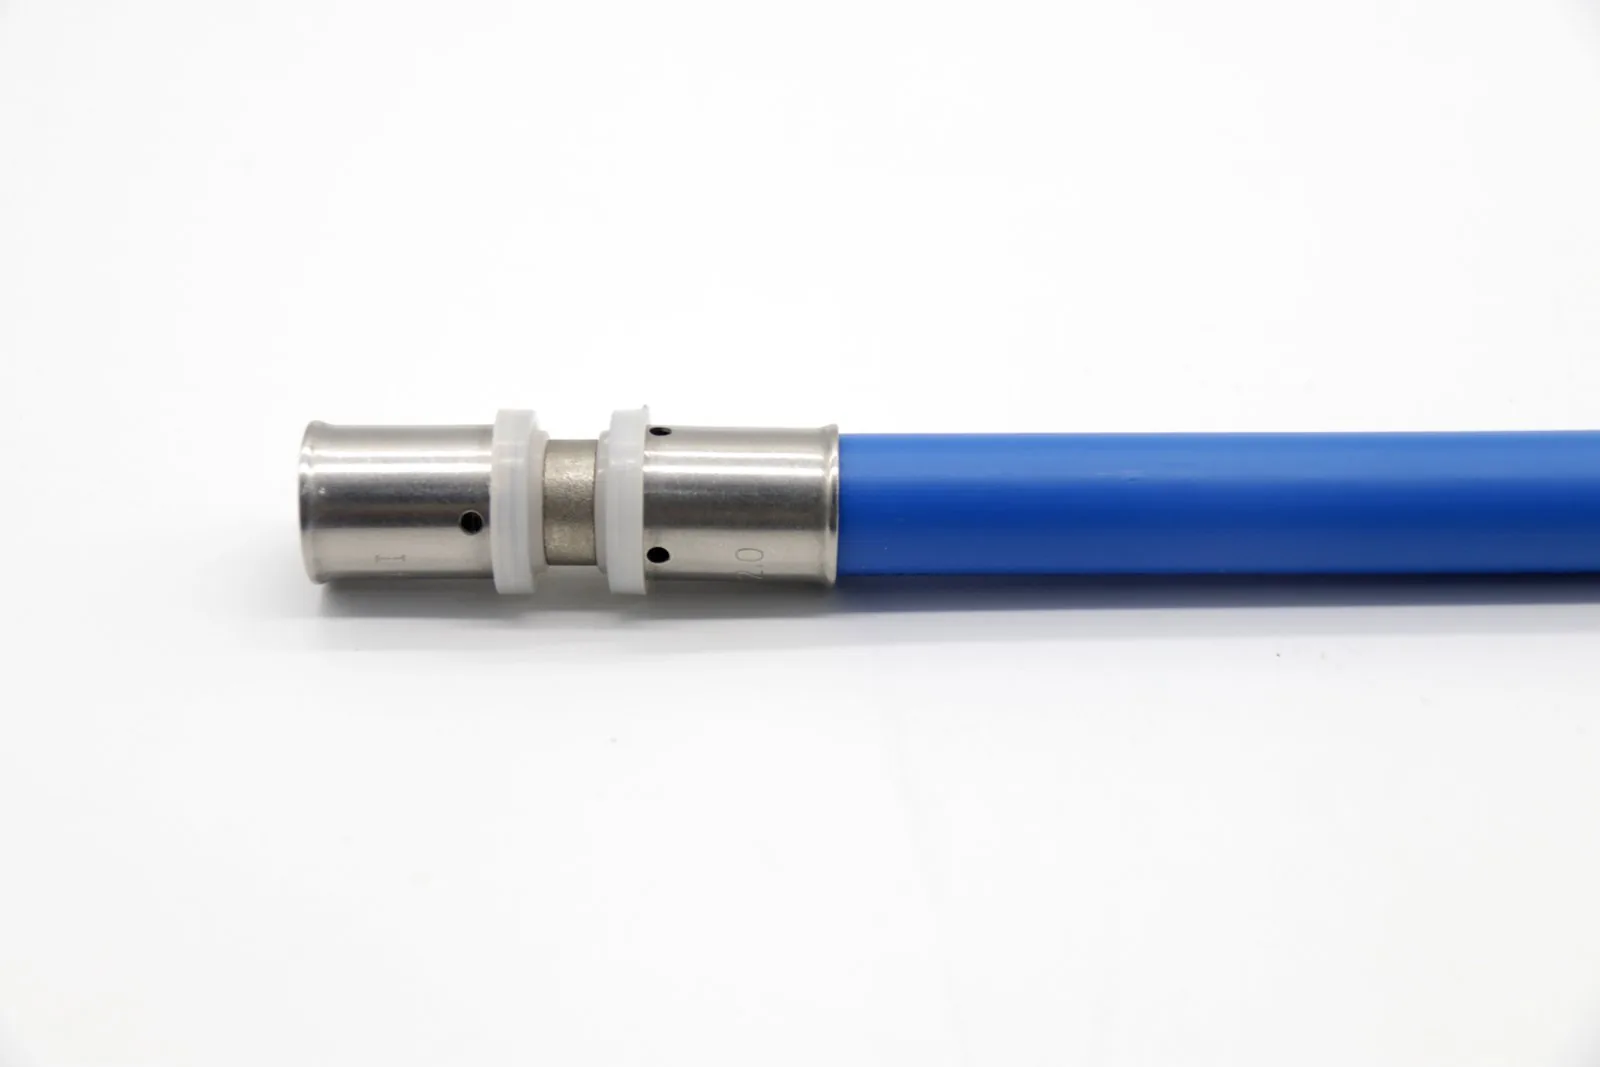
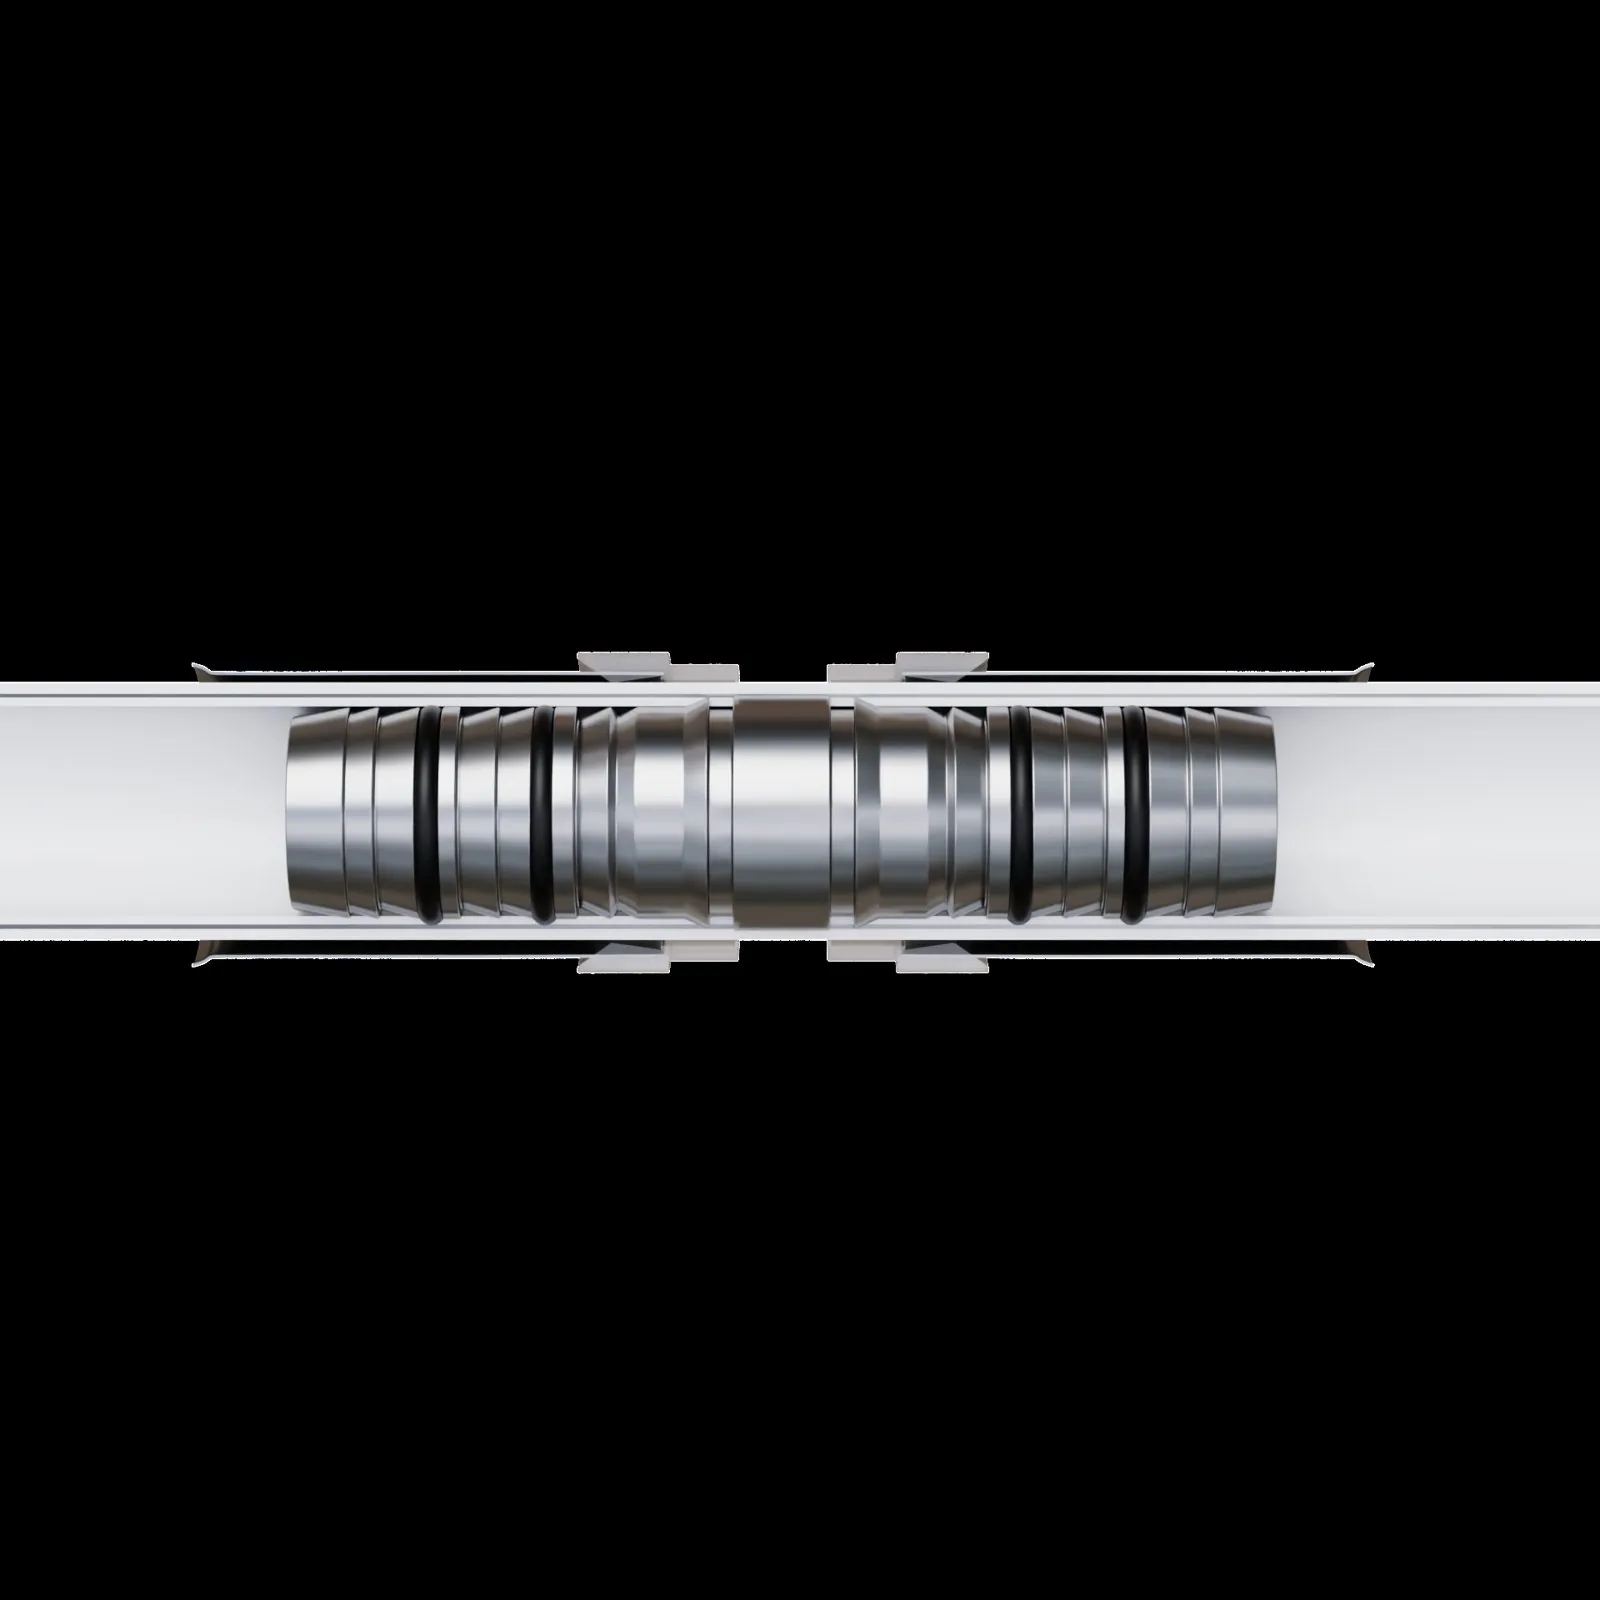
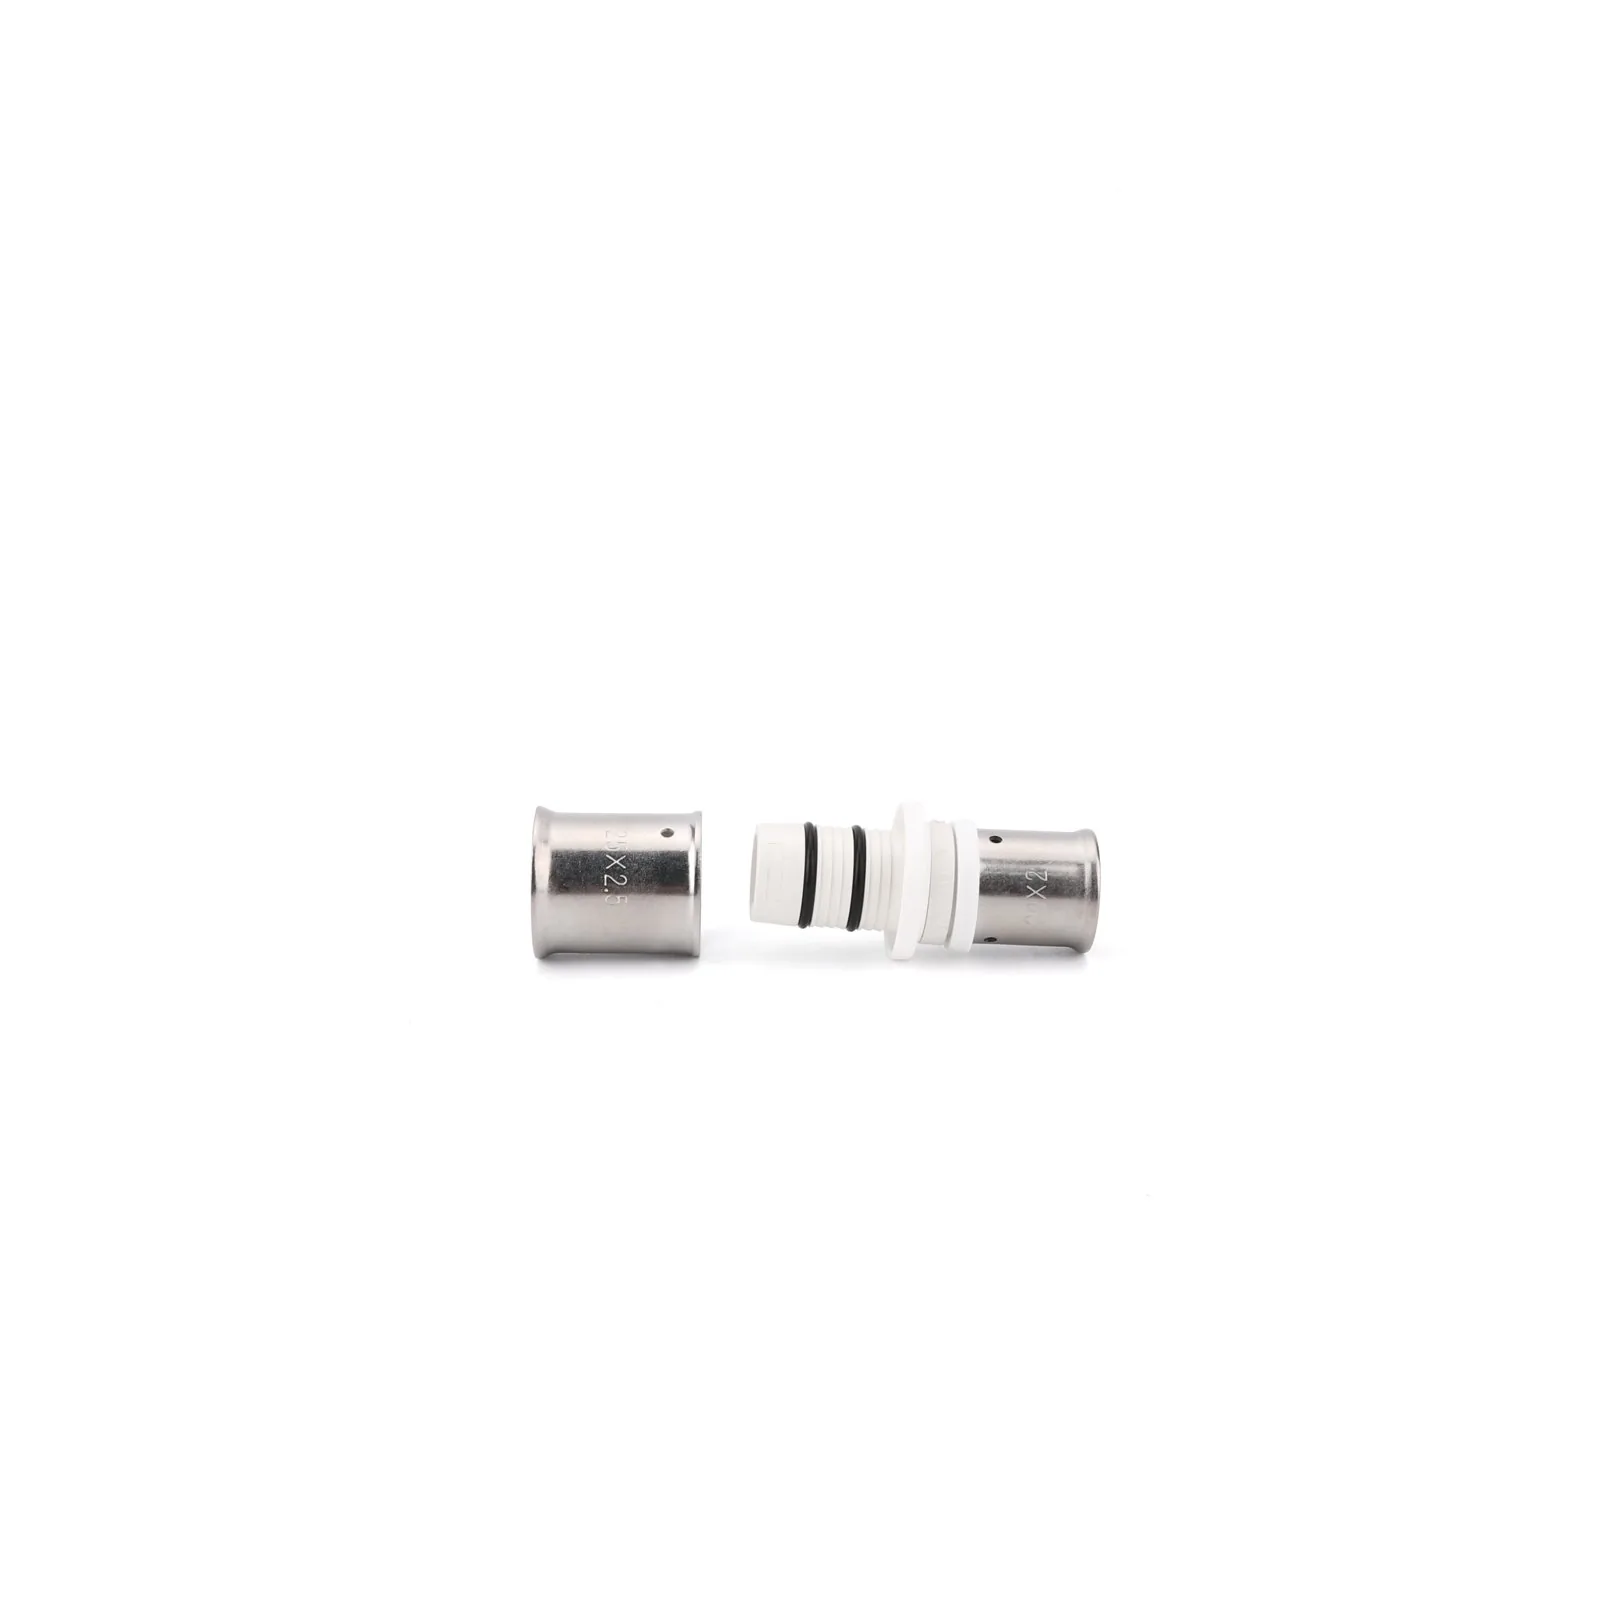
Compatibility is only half the story; the other half is whether the fitting you press to the correct contour actually holds. A Hitze multilayer press fitting is a three-element joint: a lead-free brass bore that carries the water, a stainless-steel press sleeve that grips the pipe, and a twin O-ring seal seated where the sleeve compresses. The brass is drawn from dezincification-resistant and lead-free grades — CW724R, CW511L and CW602N (DZR), with CW617N where a standard grade is specified — so the wetted metal both seals and stays safe for potable water. The stainless sleeve is what your jaw closes on; its geometry is matched to the TH, U, F or M contour the fitting is offered in.
On the process side, Hitze — a German brand producing piping systems since 1974 from a 120,000 m² base with 1,000+ employees, exporting to 118+ countries — designs the sleeve-and-O-ring geometry around the target contour and then verifies the pressed joint rather than assuming it. Finished fittings and pipe move through rows of pressure-test benches — hydrostatic verification against DIN and EN ISO requirements, checking leak-tightness of the pressed connection under sustained load, not just a quick pass at commissioning pressure. The multilayer pipe those fittings press onto is built to DIN 4726 with an oxygen-barrier layer, and the composite fitting system follows EN ISO 21003. Where a market needs it, Hitze holds German and international potable-water approvals — SKZ testing, DVGW type examination, UK WRAS material approval and an NSF / BS 6920 potable-water report — with the specific certificate numbers available on request for your submittal pack.
Two honest limits belong here. First, a certification travels with the fitting-and-contour pair it was granted on — it does not licence you to press that fitting with a different profile. Second, exact approvals vary by market and by product line, so the right move before you commit a project is to request the current certificate set for the specific fittings and sizes you intend to install rather than relying on a general claim.
How to verify a joint after pressing
There is no field gauge that can prove a pressed joint was pressed with the right contour. What exists is a three-layer check: an indicator that tells you the joint was pressed at all, a contour feature that makes an unpressed joint fail at low pressure, and a system test to a published procedure. The values below are the ones the standards and the system makers actually publish.
| Check | What you look for | Published value (bar / mbar / min) | Source |
|---|---|---|---|
| Press indicator | Foil / ring removed or sleeve window shows full press mark on every joint | Visual, no numeric value | Uponor S-Press PLUS data sheet (removable press-indicator foil) |
| Unpressed-joint detection (metal V) | Unpressed SC-Contur joint leaks visibly during the leak test | Water 1–6.5 bar; air 22 mbar–3 bar | Viega Profipress catalogue (UK) |
| Leak test, air (dry) | No pressure drop over the hold period | 150 mbar; ≥120 min per 100 L, +20 min per further 100 L | ZVSHK advisory leaflet, pressure test of drinking-water installations |
| Strength test, air | No drop over 10 min | ≤63 mm: max 3 bar; >63 mm: max 1 bar | ZVSHK advisory leaflet |
| Pressure test, water (drinking water) | Holds test pressure with no visible leak | min 11 bar, 30 min | DIN EN 806-4:2010 via ZVSHK leaflet |
Two things the table is careful not to say. First, the indicator only proves a press happened; it does not prove which contour did it, which is why the contour match belongs before the trigger, not after. Second, the drinking-water regime for the connector itself is DVGW W 534 (P) 2015-07 for the German approval and EN 1254-7:2021 for metallic press fittings — both are type-approval documents for the fitting-and-contour pair, and neither licenses a field swap of contour. Multilayer fittings sit under EN ISO 21003-3.
A worked scenario: switching a radiant-heating crew without re-tooling
Picture a radiant-heating installer running eight two-person crews across residential retrofits. Each crew carries a Novopress or REMS battery gun and a case of TH-profile jaws in 16, 20, 26 and 32 mm — bought years ago for a European multilayer system they no longer want to keep paying a premium for. The fear is real and specific: switch fitting brands, get the profile wrong, and a leak surfaces after the screed is poured and the floor is finished. That is a demolition callback, not a wipe-and-retry.
The path that avoids it is boring on purpose. First, confirm the incoming fitting is offered in the TH contour the crews already own — for Hitze multilayer press fittings, it is. Second, order a small sample lot and have one crew press test joints in each diameter, then take those joints to the pressure bench and hold them under sustained load, replicating the factory’s own hydrostatic check. Third, only after the sample joints pass do you roll the fitting into live jobs. No new guns, no new jaws, no change to how the crews physically work — the sequence at the pipe end is identical, because the contour is identical. The only thing that changed is the invoice and the margin on it.
The same logic scales up for a distributor. If your resale customers press TH and U multilayer systems, stocking a full range in those two contours plus M for the metal side lets you serve almost the entire installed base of press tools in your territory from one supplier — which is the difference between reselling a commodity and owning a system. For the underlying pipe those fittings press onto, our multilayer PEX-AL-PEX pipe is built to the same DIN and EN ISO regime as the fittings, so the pipe-and-fitting pair is warrantable as one system rather than a mix you have to defend joint by joint.
Best for, and not for
Open-contour press fittings in TH, U, F and M are the right call for:
- Contractors who already own mainstream press guns (Novopress, REMS, Klauke, Ridgid, Milwaukee) and want to change fitting brands without re-tooling.
- Distributors and wholesalers who need to serve a whole territory’s installed tool base from one full-range, certified supplier.
- Radiant-heating installers standardising a mixed fleet of crews on a single, warrantable pipe-and-fitting system.
- Private-label and project buyers who want their own brand on a fitting that presses with tools the market already carries.
They are not the automatic answer when:
- A project specification mandates a single named proprietary system end to end — there, you match the spec, not the contour.
- Your crews only own a closed “system” jaw (some Viega Smartpress / Uponor S-Press setups) and there is no budget for an open-contour jaw set.
- The job is a small one-off where a push-fit or compression joint is faster than owning press tooling at all — press economics reward volume.
Match the contour, keep your tools
If you press multilayer or metal today and want to standardise on one certified, German-brand supplier without buying new guns, Hitze press fittings come in the TH, U, F and M contours your crews already run — with a lead-free brass bore, stainless sleeve and twin O-ring seal, and certificate sets available on request for your submittal. This is aimed at trade buyers — contractors, distributors and project specifiers ordering by the carton or container, not homeowners buying a single joint. Tell us the profiles, diameters and market your crews work in, and our contractor radiant-heating supply team will confirm the matching range and send a sample lot to press-test before you commit.
Hitze is a German brand engineered in Germany and built to German DIN standards. Trade and wholesale only.
Press tools and jaws: the questions US installers ask
Search traffic on this topic splits between the European contour letters above and the US ProPress / IPS vocabulary. The four answers below translate between them.
What jaws for press fittings?
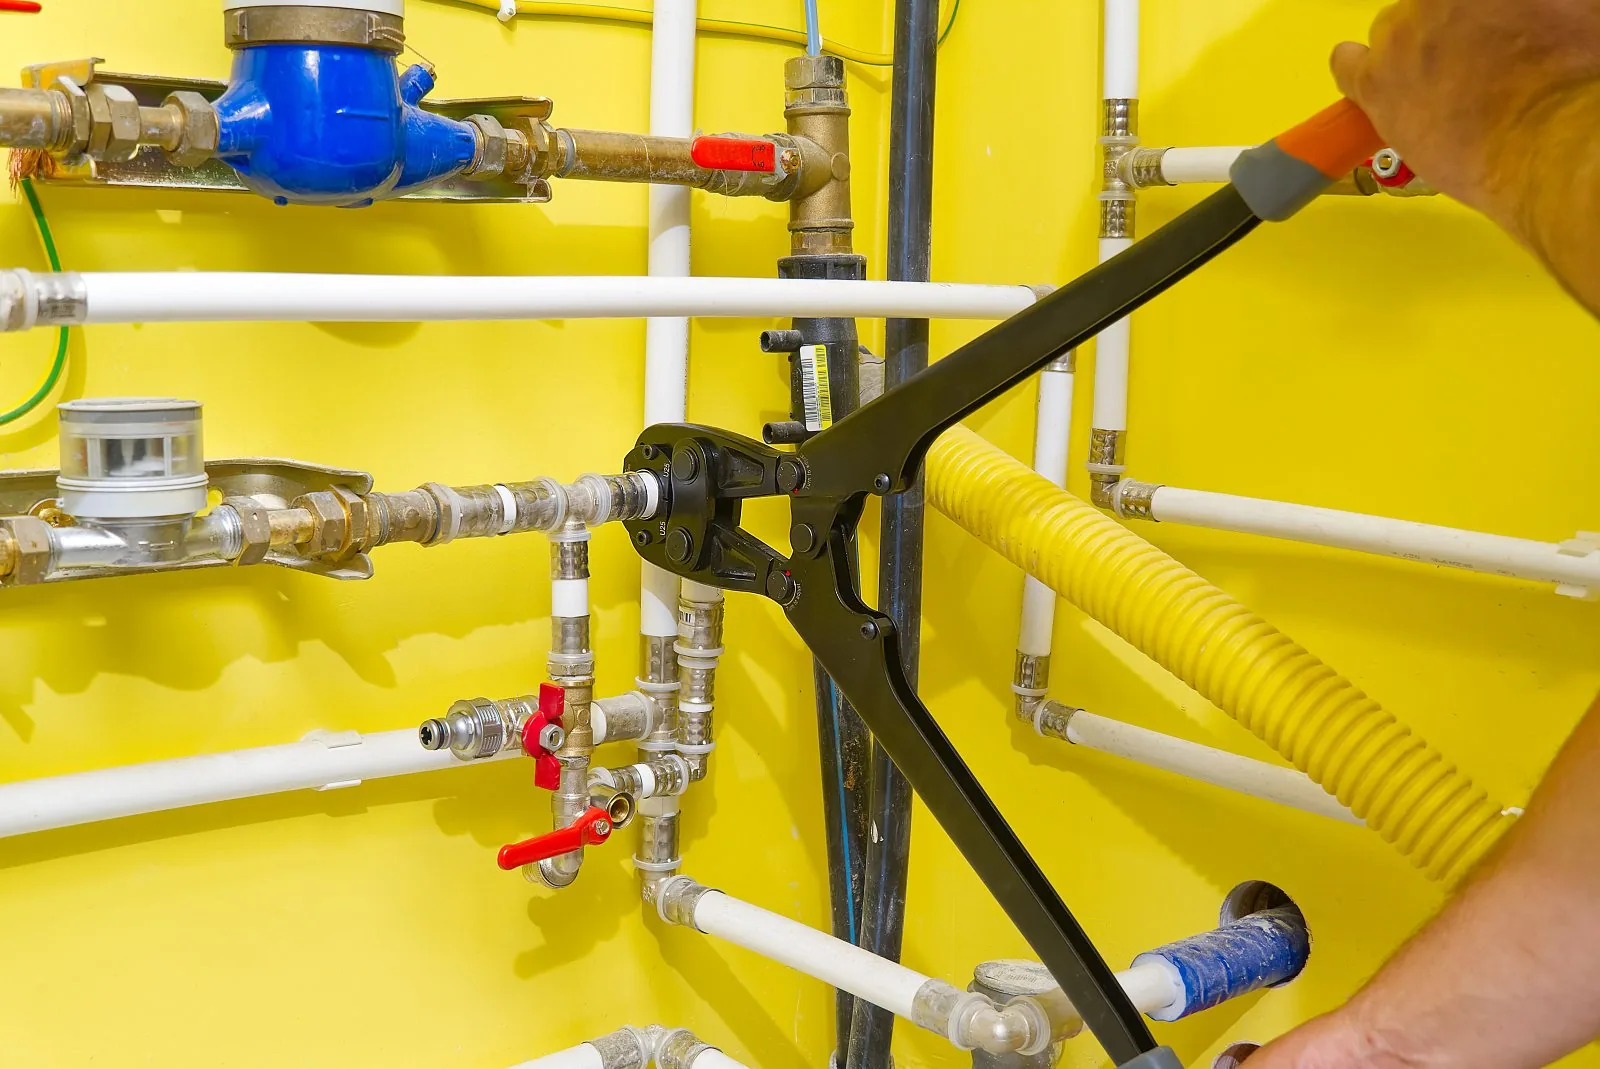
Use the jaw profile printed on the fitting’s data sheet, in the fitting’s exact diameter: TH, U, F or H for multilayer composite, M or V for copper, stainless and carbon steel in Europe, and ProPress (copper/stainless) or MegaPress IPS (steel) jaws in North America. The profile is set by the fitting maker; the tool body only supplies force. A same-size jaw in the wrong profile closes normally and produces an uncertified joint.
What are the different types of ProPress tools?
Three classes: compact tools (Viega Pressgun Picco, RIDGID RP 240/241 class) with compact jaws for ½–1¼ in, standard tools (Pressgun 6, RIDGID RP 350/351 class, Milwaukee M18 Force Logic) with standard jaws for ½–2 in, and the same standard bodies with a V2 actuator plus press rings for 1½–4 in. The tool class sets the jaw range; the jaw sets the material — ProPress jaws for copper/stainless CTS, MegaPress jaws for IPS steel.
What are the types of press tools?
By drive: manual (lever) presses, corded electro-hydraulic and battery electro-hydraulic. By force: mini/compact bodies below 32 kN for small sizes, 32 kN standard bodies for 12–108 mm with jaws to 35 mm and rings above, and 45 kN XL bodies for the largest rings. By attachment: closed jaws for small diameters, and open press rings driven by an intermediate (adaptor) jaw for large diameters. Every class takes the same profile letters — the letter, not the tool, decides fitting compatibility.
What are IPS press jaws?
IPS press jaws are jaws cut to Iron Pipe Size outside diameters, for pressing carbon-steel fittings such as Viega MegaPress onto Schedule 5–40 steel pipe, ½–2 in with standard jaws and rings. They are not interchangeable with CTS (copper tube size) ProPress jaws even at the same nominal size, because IPS and CTS tubes of the same nominal have different outside diameters. In European terms, IPS jaws are a separate metal contour, not an M or V jaw.
Frequently asked questions
Can I press a TH fitting with a U-profile jaw of the same size?
No. The tool will close and the crimp may look fine, but TH and U are different contours and are not interchangeable. The O-ring and sleeve are compressed in the wrong geometry, the joint no longer matches what the fitting was leak-tested to, and the manufacturer’s approval no longer applies. Always press a fitting with the exact profile its data sheet specifies.
Do I need a new press tool to switch fitting brands?
Usually not. Mainstream press guns from Novopress, REMS, Klauke, Ridgid and Milwaukee take interchangeable jaws and rings by profile and diameter. If a new fitting is offered in a contour your jaws already cover — such as TH or U for multilayer — you keep the gun and, at most, buy a jaw. Only closed “system” tools tie you to one brand.
What is the difference between M profile and TH or U?
They belong to different material worlds. M (and V) are metal-press contours for copper, stainless and carbon-steel systems; M is system-independent, so any M jaw presses any M fitting. TH, U, F and H are composite contours for multilayer PEX-AL-PEX and PE-RT pipe, and each is tied to specific systems. Never carry a metal-press habit over to a composite fitting or vice versa.
Which jaw profiles do Hitze press fittings use?
Hitze press fittings are offered in the mainstream TH, U, F and M contours, so a crew that already presses multilayer or metal can adopt them without re-tooling. They are built with a lead-free brass bore, a stainless-steel press sleeve and a twin O-ring seal, and are supplied to trade and wholesale buyers by the carton or container.
Are Hitze press fittings made in Germany?
Hitze is a German brand — GERMANY Hitze Industry Co., Ltd., holding German Trademark Reg. No. 30 2020 005 484 — engineered in Germany and built to German DIN and EN ISO standards. The fittings are produced with lead-free DZR brass grades and verified on hydrostatic pressure benches, and they carry potable-water approvals such as SKZ, DVGW, WRAS and NSF/BS 6920, with certificate numbers available on request.
How do I confirm a fitting is compatible before I order a container?
Check three things on the fitting’s data sheet: the approved pressing contour (TH, U, F, M), the diameters offered, and the certification set for your market. Then request a sample lot, press test joints in each diameter with your own tools, and verify them on a pressure bench under sustained load before committing volume. If a comparable system was previously specified, our Viega alternative overview shows how the contour-match logic applies when you switch.


